2026 Top Welding Flanged Pipe Suppliers How to Choose?
Choosing among the 2026 top Welding Flanged Pipe suppliers requires more than comparing catalog prices. A polished website proves little. Buyers need evidence of manufacturing control, material traceability, and dependable delivery. The strongest suppliers can identify steel heat numbers, flange dimensions, welding procedures, and inspection records without hesitation.
John C. Lippold, a respected welding metallurgy expert and author, has stated, “Weldability depends on the material, the welding process, and the service conditions.” This principle applies directly to Welding Flanged Pipe selection. A supplier may produce attractive welds, yet still fail when temperature, pressure, corrosion, or vibration changes. Ask whether the supplier qualifies procedures under ASME Section IX or an equivalent standard. Review radiographic, ultrasonic, or magnetic particle testing where the application requires it. Check compliance with ASME B16.5, ASME B16.47, EN standards, or project-specific specifications.
Small details matter. Request EN 10204 3.1 certificates, dimensional reports, coating records, and packing photographs. Confirm the supplier’s experience with carbon steel, stainless steel, duplex steel, or specialized alloys. Visit the factory when possible. Watch how pipes are aligned before welding. Notice whether finished flanges are protected from impact and contamination.
A low quotation can hide future costs. It might reflect weaker inspection, uncertain tolerances, or poor after-sales support. Still, no supplier is perfect. Even reputable factories can miss a deadline or misunderstand a drawing. This guide compares leading suppliers through quality systems, welding capability, inspection transparency, customization, communication, and total project value. The goal is not to find the cheapest source. It is to find a partner whose Welding Flanged Pipe performs reliably in the real installation.
What Are Welding Flanged Pipes and Where Are They Used?
Welding Flanged Pipes: What They Are and Where They Are Used
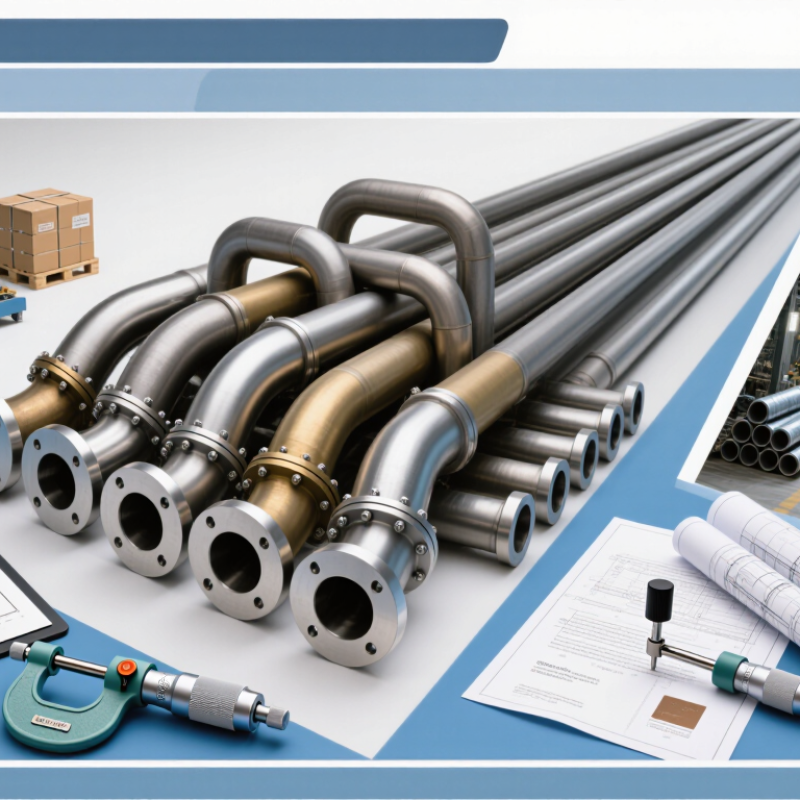
A welding flanged pipe is a pipe joined to a flange by welding. The flange creates a bolted connection between pipes, valves, pumps, and other equipment. Welding neck flanges support high-pressure service because their tapered hub transfers stress gradually. Slip-on flanges are easier to install, but they usually suit less demanding conditions.
These assemblies appear in water treatment plants, power stations, chemical facilities, refineries, and marine systems. The United Nations World Water Development Report 2024 states that agriculture represents about 70% of global freshwater withdrawals. This demand supports extensive irrigation and water-treatment networks, where flanged joints simplify inspection and maintenance. Energy systems also use them widely. The International Energy Agency reported that global energy investment was expected to exceed 3 trillion dollars in 2024, increasing demand for dependable piping connections.
Standards matter. ASME B16.5 defines flange dimensions, pressure classes, materials, and testing requirements for many industrial applications. A qualified supplier should provide material certificates, welding procedure records, dimensional reports, and pressure-test evidence. Check the pipe schedule, corrosion allowance, gasket type, bolt material, and operating temperature. Small details matter.
Field experience also exposes a weakness. A correctly rated flange can still leak after poor alignment or uneven bolt tightening. I may be overly cautious, but supplier selection should include traceability and welding inspection, not price alone. Some projects underestimate thermal expansion. That mistake becomes expensive.
2026 Top Welding Flanged Pipe Suppliers: How to Choose? — What Are Welding Flanged Pipes and Where Are They Used?
| Selection Dimension | What to Evaluate | Relevant Technical Data | Supplier Verification Points |
|---|---|---|---|
| Product Definition | Understand the pipe-and-flange assembly | A welding flanged pipe is a pipe section permanently joined to a flange by welding. The flange provides a bolted connection to another flange, valve, pump, vessel, or fitting. Common welded configurations include weld-neck flanges, slip-on flanges, socket-weld flanges, and blind flanges used with a pipe spool. | Confirm whether the supplier provides loose flanges, welded pipe spools, or complete fabricated assemblies. Check drawings, weld details, and dimensional tolerances before ordering. |
| Primary Applications | Match the assembly to the service environment | Typical applications include oil and gas piping, chemical processing, water treatment, power generation, shipbuilding, district energy, HVAC, mining, fire-water systems, and industrial compressed-air lines. | Ask for relevant fabrication experience in the same service category, especially for corrosive, high-temperature, low-temperature, toxic, or cyclic-pressure applications. |
| Pipe Material | Select material according to fluid, temperature, and corrosion risk | Carbon steel ASTM A106 is commonly used for seamless carbon-steel pipe in high-temperature service. ASTM A53 is widely used for general-purpose pressure and mechanical applications. Stainless steel ASTM A312 covers seamless and welded austenitic stainless-steel pipe for corrosive and high-temperature service. Low-temperature steel ASTM A333 covers seamless and welded steel pipe for low-temperature service. | Verify material certificates, heat numbers, chemical composition, mechanical properties, and traceability from raw material through final assembly. |
| Flange Material | Ensure compatibility between flange and pipe | Common flange materials include forged carbon steel, stainless steel, alloy steel, and duplex stainless steel. The flange material should be compatible with the pipe material, design temperature, pressure, corrosion conditions, and applicable piping code. | Check the flange material grade, heat treatment condition, impact-test requirements, corrosion allowance, and compatibility with the selected gasket and bolts. |
| Flange Design | Choose the correct connection type | Weld-neck: Preferred for high-pressure, high-temperature, and cyclic loading because the tapered hub transfers stress gradually. Slip-on: Easier to fit and commonly used in moderate-duty systems; normally requires internal and external fillet welds. Socket-weld: Often used for smaller nominal pipe sizes and higher-pressure services. Blind: Used to close a pipe end, nozzle, or branch connection. | Confirm flange type, bore, hub dimensions, facing, wall thickness, weld-end preparation, and whether the design is suitable for vibration and thermal cycling. |
| Size Range | Match nominal pipe size and wall thickness | ASME B16.5 generally covers flanges and flanged fittings from NPS 1/2 through NPS 24. ASME B16.47 covers large-diameter flanges from NPS 26 through NPS 60. Actual available sizes depend on the selected standard, material, pressure class, and fabrication capability. | Provide nominal size, outside diameter, wall thickness or schedule, flange bore, face-to-face length, and spool overall length. Confirm dimensional inspection records. |
| Pressure Rating | Use the correct pressure-temperature rating | ASME flange classes commonly include Class 150, 300, 400, 600, 900, 1500, and 2500. The allowable pressure depends on material group, design temperature, flange standard, and pressure class; the class number is not a direct pressure value in bar or MPa. | Request the design pressure, design temperature, operating pressure, test pressure, material group, and applicable pressure-temperature rating table. Do not select a class from pressure alone. |
| Flange Standards | Maintain dimensional and interchangeability requirements | Common standards include ASME B16.5 for pipe flanges and flanged fittings, ASME B16.47 for large-diameter flanges, EN 1092-1 for steel flanges, and JIS B2220 for Japanese industrial flange dimensions. These systems are not automatically interchangeable. | Specify one complete dimensional system, including standard, nominal size, pressure designation, facing type, bolt-hole pattern, bore, and tolerances. |
| Pipe Standards | Select a pipe specification suitable for the service | Frequently specified standards include ASTM A106 for seamless carbon-steel pipe, ASTM A312 for stainless-steel pipe, ASTM A333 for low-temperature pipe, ASTM A790 for duplex stainless-steel pipe, and API 5L for line pipe used in many pipeline applications. | Confirm product form, seamless or welded construction, grade, dimensions, supplementary requirements, testing, and whether the pipe standard is permitted by the project piping code. |
| Welding Process | Control weld quality and repeatability | Common processes include GTAW/TIG for root passes and thin-wall or stainless-steel work, GMAW/MIG for productivity, SMAW for field or repair work, and SAW for suitable large-diameter fabrication. Process selection depends on material, thickness, access, production volume, and code requirements. | Request qualified welding procedure specifications, procedure qualification records, welder qualifications, preheat requirements, interpass-temperature controls, and post-weld heat-treatment records where required. |
| Weld Inspection | Verify weld integrity before shipment | Inspection methods may include visual testing, liquid penetrant testing, magnetic-particle testing, radiographic testing, and ultrasonic testing. The required method and acceptance criteria depend on the piping code, service category, material, weld type, and project specification. | Confirm inspection percentage, acceptance standard, inspection personnel qualification, nonconformance procedure, repair records, and availability of final inspection reports. |
| Gasket and Bolting | Prevent leakage at the flanged joint | Gasket selection depends on fluid, pressure, temperature, flange facing, and chemical compatibility. Bolting must be selected for strength, temperature, corrosion exposure, and the applicable standard. Flange face condition and controlled bolt tightening are critical to sealing performance. | Require gasket type and dimensions, bolt grade, nut grade, washer requirements, tightening procedure, torque or tension values, and flange-face protection during transport. |
| Temperature Capability | Account for thermal expansion and material limits | Service temperature affects allowable pressure, gasket performance, bolt preload, thermal expansion, impact toughness, and weld behavior. Carbon steel, stainless steel, alloy steel, and low-temperature grades have different operating limitations. | Submit design and operating temperature ranges, minimum design metal temperature, impact-test requirements, heat-treatment records, and pressure-temperature calculations where applicable. |
| Corrosion Resistance | Match metallurgy to the process fluid | Corrosion risks may include general corrosion, pitting, crevice corrosion, erosion, galvanic corrosion, and stress-corrosion cracking. Stainless steel, duplex stainless steel, alloy steel, coatings, linings, and corrosion allowance may be considered depending on the service. | Provide fluid composition, chloride level, pH, velocity, contaminants, and concentration. Check material recommendations, passivation or pickling requirements, coating records, and surface-finish specifications. |
| Dimensional Accuracy | Ensure fit-up during installation | Important dimensions include pipe outside diameter, wall thickness, flange outside diameter, bolt-circle diameter, bolt-hole diameter, number of holes, flange thickness, bore, face-to-face length, and angular alignment. | Review approved drawings, dimensional inspection plans, flange rotation and orientation requirements, end squareness, weld shrinkage controls, and final fit-up measurements. |
| Testing and Documentation | Create a complete quality dossier | A typical dossier may contain material certificates, dimensional reports, welding records, non-destructive examination reports, heat-treatment records, pressure-test certificates, coating records, marking details, and packing lists. | Confirm document format, inspection and test plan, document approval workflow, traceability requirements, retention period, and whether original or digitally signed records are required. |
| Pressure Testing | Demonstrate leak-tightness and structural integrity | Hydrostatic testing is widely used for pressure piping, while pneumatic testing may be permitted only under controlled conditions because stored compressed-gas energy creates greater safety risk. Test pressure and hold time must follow the applicable code and project specification. | Ask for the approved test procedure, test medium, calibrated gauges, test pressure, duration, test boundary, safety controls, acceptance criteria, and signed test certificate. |
| Manufacturing Capacity | Confirm the supplier can meet quantity and schedule | Capacity depends on available forming, machining, welding, heat-treatment, non-destructive examination, coating, and pressure-testing equipment. Large-diameter or high-alloy assemblies generally require more specialized production resources. | Request a realistic production schedule, capacity statement, equipment list, subcontractor controls, sample lead times, and contingency plans for raw-material or inspection delays. |
| Packaging and Delivery | Protect the assembly during transportation and storage | Flange faces should be protected from impact, corrosion, moisture, dirt, and distortion. Carbon-steel assemblies may require temporary corrosion protection, while stainless-steel assemblies should be protected from contamination by carbon-steel tools or packing materials. | Specify end caps, flange-face protectors, lifting points, moisture protection, preservation period, crate dimensions, marking, center of gravity, and handling instructions. |
| Commercial Comparison | Compare total value rather than unit price alone | Total cost includes pipe and flange materials, machining, welding, inspection, testing, coatings, documentation, packaging, freight, duties, installation preparation, and potential leakage or rework costs. | Use the same technical specification and scope for every quotation. Compare exclusions, inspection costs, delivery terms, warranty, payment conditions, replacement policy, and change-order rates. |
| Final Supplier Shortlist | Choose the supplier with the strongest technical fit | A suitable supplier should demonstrate material traceability, qualified welding, code-compliant fabrication, reliable inspection, dimensional control, pressure testing, transparent documentation, and consistent delivery performance. | Rank suppliers using weighted criteria such as technical compliance, quality documentation, inspection capability, lead time, total cost, production capacity, safety record, and after-sales support. Approve the final supplier only after technical clarification is closed. |
Get in touch with us,
We will contact you shortly!
What is the difference between Unline(Non-Epoxy Coated) or Lining(Epoxy Coated) Metal Drum?

What are Unline(Non-Epoxy Coated) and Lining(Epoxy Coated) drums compatible with?
What is the difference between Grade A and Grade B Metal Drum ?
What content is suitable to fill in a Recon Grade A or Grade B Drum?
What is the difference between Open Top and Close Top Drums and their usage?
What type of content are Metal or Plastic Drums suitable for?
Will there be any contamination in the reconditioned metal, plastic drums or IBC tanks?
What is the drum gauge(thickness) and weight for reconditioned metal drums?
Do you sell New Packaging Products too?
What additional services do you provide apart from selling reconditioned and new containers.?
Do you offer labelling and silkscreen on the containers ?
Are you able to ship overseas ?
Leading the Way
to Carbon Neutrality